Food safety
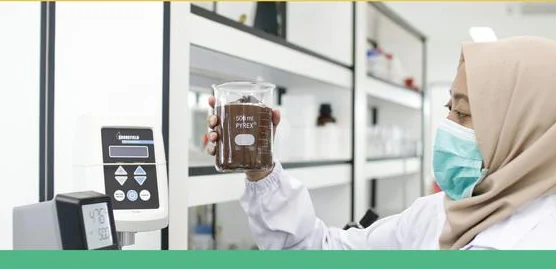
A unified quality and food-safety system covers raw-material control, process supervision, finished-product testing, storage and transport.
Research, application testing, quality control and production support connected around your product.
Our teams support product developers and buyers with practical answers about performance, safety and production.
A unified quality and food-safety system covers raw-material control, process supervision, finished-product testing, storage and transport.
Production lines from Buhler, Hacos, Royal Duyvis Wiener, Sollich and SACMI support stable quality and high automation.
Two R&D centers in Hangzhou and Shanghai include application laboratories for frozen desserts, bakery and broader food systems.
We translate application demands into ingredient specifications through sensory, formulation and process testing.
Each project is scoped around the technical task, target launch date and commercial scale.
Define the application, sensory goal, process limits, market requirements and volume.
Select a starting product and adapt the composition to the agreed specification.
Prepare application samples and review taste, texture and handling performance.
Confirm quality documents, process fit, packaging and commercial requirements.
Move into production with consistent specifications and agreed delivery planning.
Automated manufacturing, digital process records and rigorous product checks reduce food-safety risk. Our monitoring programs cover fine particle size, moisture loss, acid value, total plate count and other quality indicators.
Tell us where the product will be used, the process it must survive and the experience your customer should have.